Get in touch with Tengyang Company

Surface Energy: Meaning, Units and Bonding Relevance Blogs
A dyne test is a testing method that screens whether a chosen test liquid reaches adequate wetting tension and spreads over a test surface. It may indicate if further investigation into the process is warranted to check for cleaning or treatment related issues. It doesn’t determine if the final adhesive is secure or if the coating has adequate durability or if there are production losses.
What it readsWetting behavior in dynes/cm under one liquid, surface and observation method.
What it cannot proveA universal bond-strength threshold or long-term adhesion result.
Best useScreening, lot comparison and treatment-age checks tied to an application test.
Illustrative record snapshot (not a universal specification): write down the procedure-defined observation window, mapped locations, labelled test-liquid level, tested side and treatment age. Record the test-liquid batch and open date, controlled environment when relevant, stroke method and operator. Link the screen to the application-test reference and note any storage checkpoint that the qualification plan actually defines. Add film thickness only when it affects the comparison. These are record fields, not universal acceptance limits.
What a dyne test actually measures
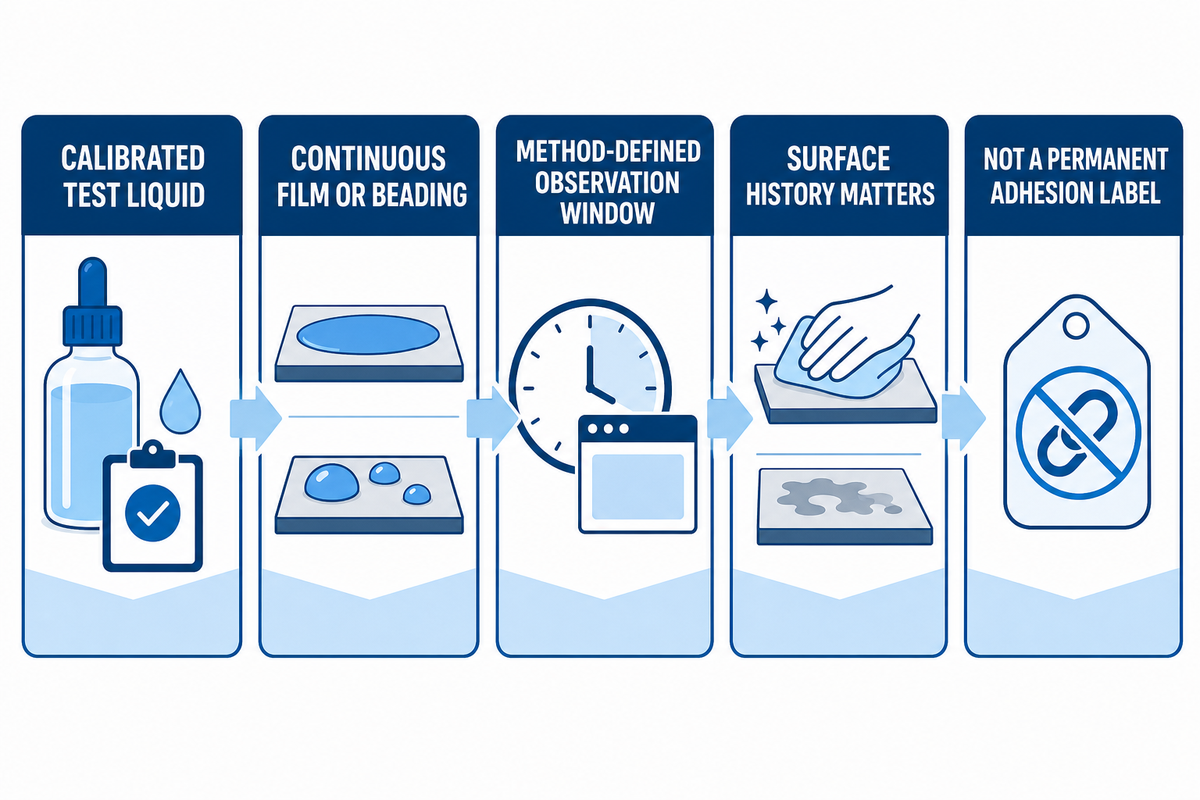
An operator runs a dyne test by applying a calibrated test liquid and recording how it behaves during the observation window defined by the test product or method. The operator may draw a short line with dyne test ink and observe whether the liquid forms a continuous film on the surface or beads up.
Continuous coverage suggests that the selected level is compatible with the surface response under that procedure. If the line beads or breaks, the selected liquid may be too energetic for the surface under that procedure.
The wetting-tension reading of a surface may change over time. A polymer surface may show one value immediately after treatment and another after storage, handling or exposure to additives, even before the product is used. Environmental conditions and elapsed time can affect the reading, which is normally expressed in dynes per centimetre and is numerically equivalent to millinewtons per metre; the number belongs to the test liquid, material, surface history and observation rule, not to a permanent adhesion label.
Scope anchor ASTM D2578 is not a treatment for achieving wet tension; it is a method reference for measuring wetting tension on low- and high-density polyethylene and polypropylene films. This scope anchor is not a practice or an acceptance criterion for films, coating, papers, metals, or molded parts. Assess the material and current edition before issuing any statement that the result meets ASTM requirements.
Scope boundary: Polyolefin films are the most simple and efficient substrates for establishing a dyne correlation. Absorption, geometry and chemical interaction on other substrates may change the continuity picture. When a surface is treated to achieve a dyne level, record treatment time, dyne-measurement time and bonding or coating application time before comparing continuity. A reading is only transferable when those substrate and time variables have been qualified together.
Working definition: read a dyne result as “this surface accepted this test liquid for this time under this method.” That wording keeps the observation useful without turning it into an unsupported adhesive guarantee.
Dyne level, surface energy, surface tension and wettability are related, not interchangeable
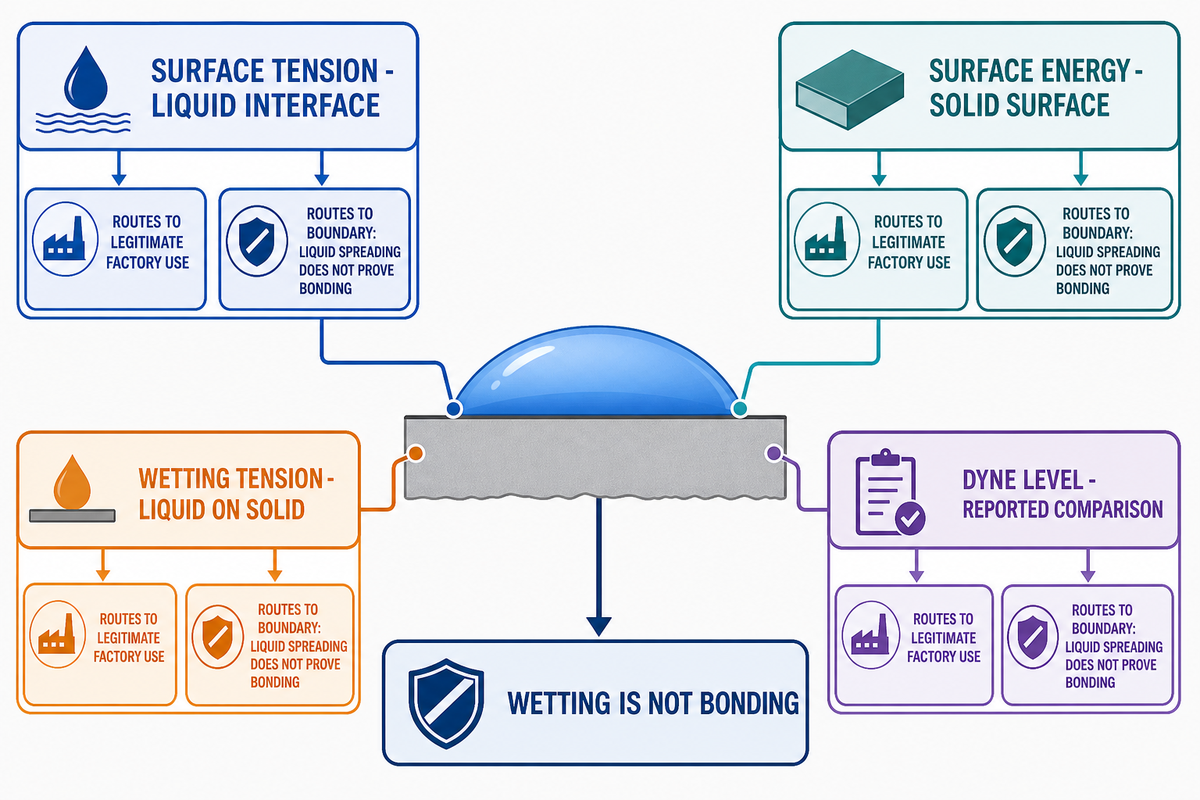
A surface energy measurement is not interchangeable with surface tension, wetting tension, or a reported dyne level, even though production teams often use these terms as synonyms. In reality, each of these terms describes a particular element at the factory interface.
In this context, wetting describes the interaction between a liquid and a solid under the stated conditions; it is not the same as bonding. In a system made up of a liquid and a solid, the behavior of the liquid and the solid may differ in relation to equilibrium and balance. The interaction of a liquid and a solid may be described using a dyne solution. In such a case, a comparison between the two may be recorded. In other words, surface tension may support liquid spreading on a solid, but it does not prove that the liquid is bonded to the solid.
| Term | Where it belongs | What a production team can use it for | What it does not settle |
|---|---|---|---|
| Surface tension | Liquid interface | Compare the test liquid selected for a method | Whether a particular adhesive will survive service |
| Surface energy | Solid surface | Discuss material and treatment changes | A single universal pass/fail number for all products |
| Wetting tension | Practical liquid-on-solid response | Screen whether a liquid spreads for the stated time | Cohesive strength, peel strength or aging life |
| Dyne level | Reported comparison value | Trend lots, treatment settings and surface cleanliness | Final bond quality without an application test |
For more detail on interfacial terms and their relevance to bonding, see surface energy: meaning, units and bonding relevance. Use that page as the theory handoff; keep this article focused on reading and governing the screen.
Reading capsule: Dyne numbers are signals of the method in question and should not be interpreted on their own. Write down the test-liquid family, surface, timing and material. Compare results only when those conditions match.
How to run a repeatable dyne test with pens or inks
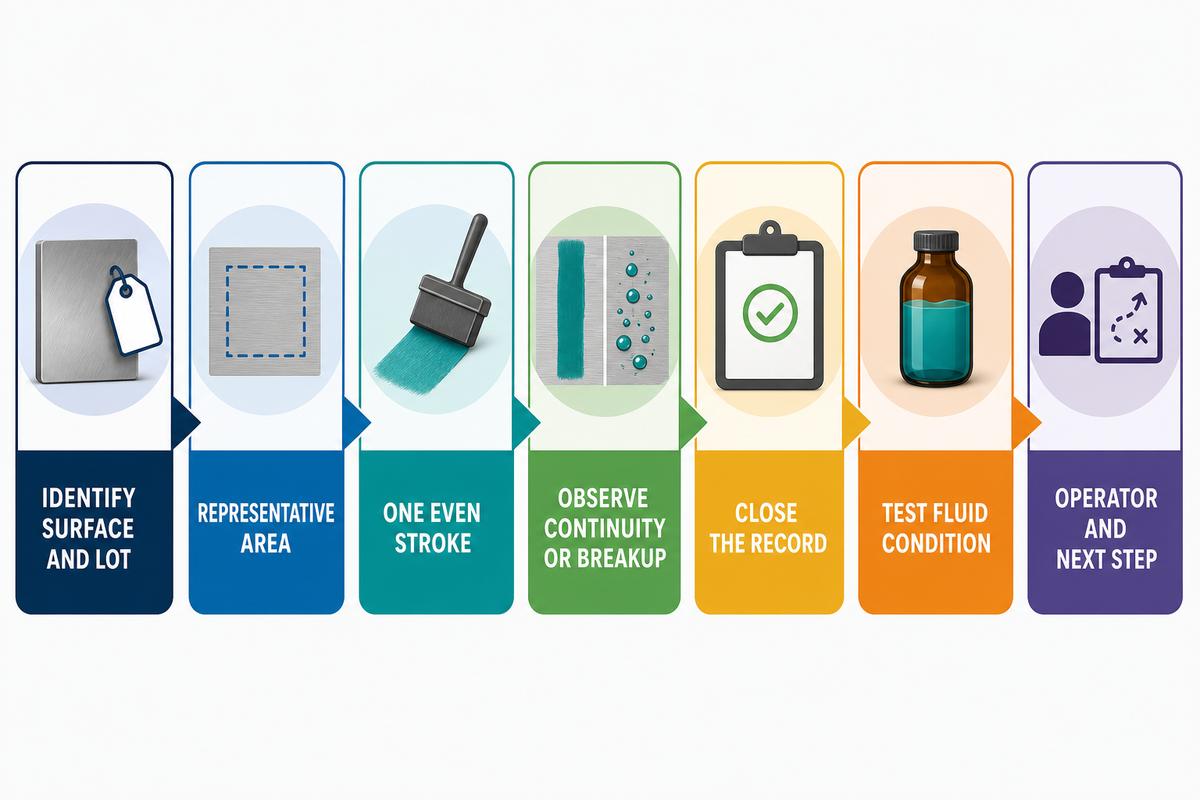
A repeatable dyne test requires a representative area, a clean instrument and an operator who follows a written observation rule. Several procedures may be acceptable when their conditions are controlled and recorded. The goal isn’t to produce an aesthetic result; it is to repeat a consistent small experiment on each lot.
- For a production lot, identify the tested surface and state whether it is a polymer or coating, and record the lot and treatment; because contamination or a wrong side can trigger a failed factory quality hold, note the applicable method, its product-defined observation window, and the operator’s repeat-test decision. The state of the surface of the film is important.
- During the experimental determination of the adhesion of a film to a substrate, the process window is determined by the available adhesives, coating or ink. Don’t copy a competitor’s “38 dyn/cm pass” without matching material and application.
- Don’t polish the surface; surface preparation should remove surface contaminants without making the test zone shiny.
- Make one even stroke. Evenly distribute the dispersion.
- During the experiment, record whether the last ink swath remains wetted for the stated window and note any irregularities on the film. State if the film remains continuous, or if it breaks or beads.
- Test at least three points when the work instruction requires a three-location screen, especially where the web, molded surface, or treatment head may be non-uniform. Mark the machine direction and cross-direction where applicable.
- Close the record. Document the condition, grade or batch of the pen or ink, the test operator, environmental conditions (temperature and relative humidity) and the next step to be taken.
Brighton Science’s commercial guidance says a meaningful test requires a surface controlled for contaminants.
Common mistake: drawing repeatedly over the same spot and choosing the most stable-looking line. That can deposit liquid, remove weak contamination or change the surface. One controlled pass per location is easier to audit.
How to read continuity, breakup and borderline behavior
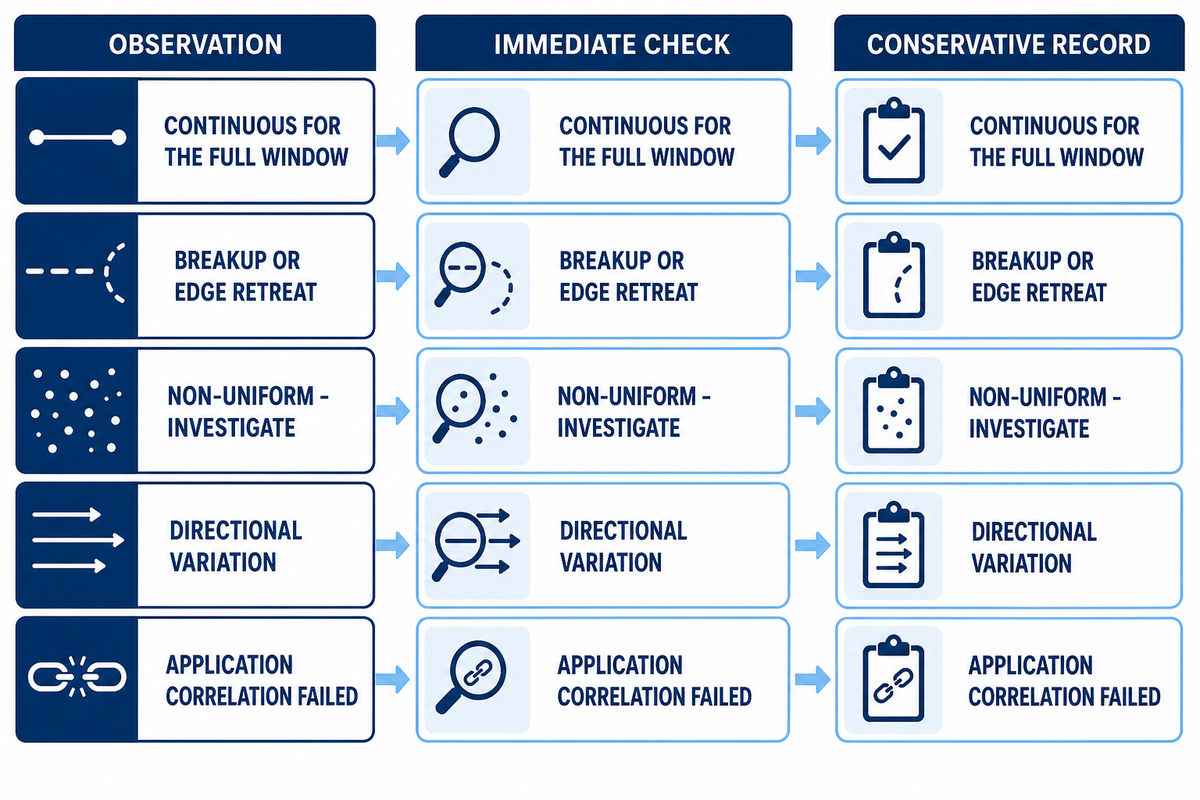
After the pen or ink procedure, don’t evaluate the result only as “wet” or “dry”; because a borderline line can hide contamination or continuity failure, record the product- or method-defined observation window and repeat-test decision. The shape and timing of the test liquid provide relevant evidence. If a line disintegrates to leave a dry area before the product- or method-defined observation period ends, the line wasn’t continuous for that procedure. A borderline result must be resolved with a repeat test, and a pass must not be given until the operator has recorded the method, observation window and contamination check.
| Observed behavior | Likely reading | Immediate check | Record wording |
|---|---|---|---|
| Continuous line for the full window | Selected level is compatible with the surface response | Confirm ink condition and timing rule | “Continuous at X dynes/cm for Y seconds” |
| Line breaks quickly | Selected liquid is too high for the observed wetting response | Repeat on a clean adjacent area | “Breakup at X dynes/cm after Y seconds” |
| Edge contraction, centre remains | Borderline or locally heterogeneous response | Check surface uniformity and stroke pressure | “Borderline; edge retreat observed” |
| Random islands or pinholes | Contamination, texture, porosity or application artifact may be involved | Compare with a second location and blank control | “Non-uniform; investigate before disposition” |
| All levels bead immediately | Surface may be low-energy, contaminated or incompatible with the ink system | Verify ink family and material identity | “No level accepted; method review required” |
| All levels spread unusually fast | Liquid may be old, contaminated or too low for the range | Check storage, cap and reference surface | “Unexpected complete spread; control check failed” |
| Machine direction passes, cross direction fails | Treatment or surface composition may be non-uniform | Map the web or part rather than averaging blindly | “Directional variation present” |
| Freshly treated sample passes; stored sample fails | Surface recovery, migration or handling may be changing wetting | Compare elapsed time and storage condition | “Age-linked drift suspected” |
| Dyne passes but bond test fails | Wetting was adequate; another bond variable controls the result | Review adhesive, cure, pressure, cleanliness and failure mode | “Screen passed; application correlation failed” |
Film-Side Wetting Trace: Consider test stability as the indicator that determines the test level; move from low to higher levels, stop at the first stable continuity, and confirm that level at multiple locations.
Why a higher dyne result does not automatically mean stronger adhesion
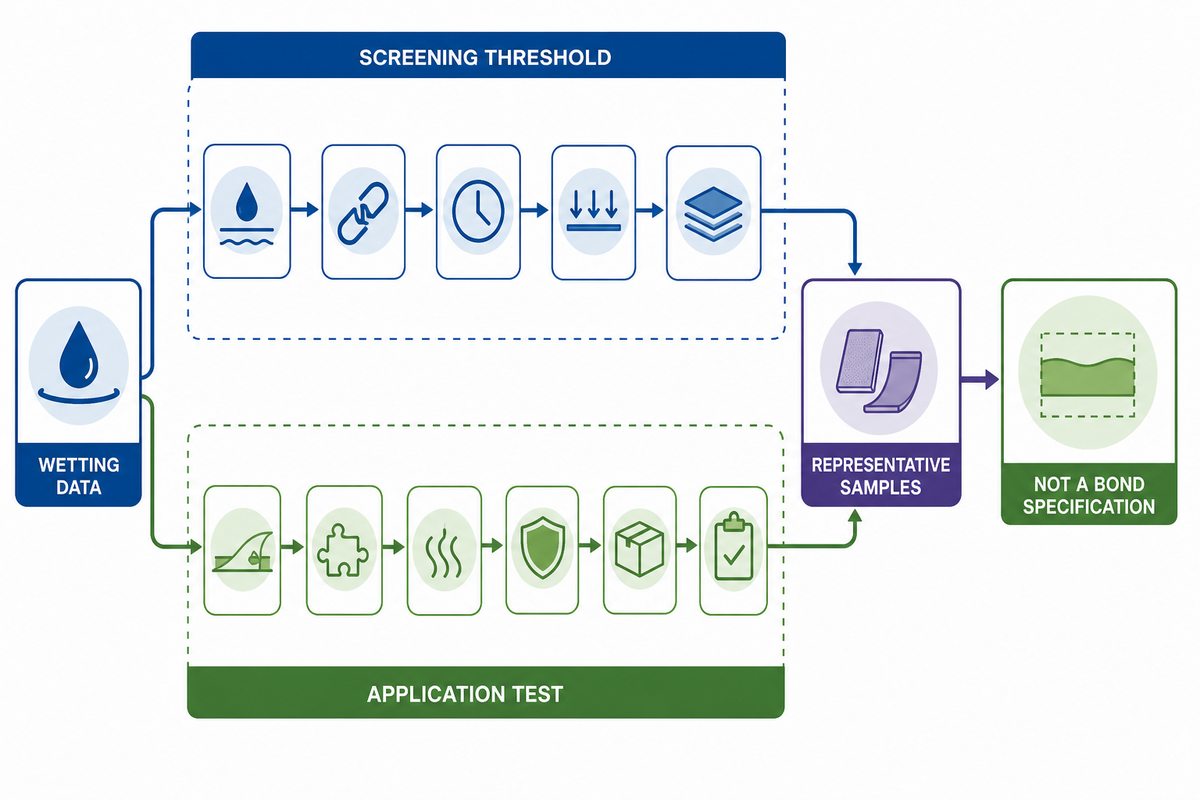
The limitations of dyne testing include other factors that affect wetting tension data, such as chemical composition, contact time, viscosity, surface texture, service condition, and operator skill and experience. The surface may be sufficiently wet out by test ink and still not give adequate bond strength; adequate adhesion must be determined by the application test because an incompatible adhesive or weak boundary layer can control the result.
The most far reaching limitation of dyne test states that dyne’s test results should be interpreted with caution and shouldn’t be considered as definitive test results to evaluate end product acceptance. Acceptance limits should be determined by actual experimentation because a factory release decision needs an application result, not a generic 38 dynes/cm guideline outside its ASTM scope.
Decision rule: if the dyne result changes and the application result changes in the same direction, you have a useful correlation for that material and process. Until that correlation is demonstrated, call the dyne value a screening threshold, not a bond specification.
Enercon also notes, in the context of an acceptance test, that a higher Dyne test result doesn’t guarantee the end product will meet the specification. Therefore, it’s prudent to define an acceptance window based on representative samples, rather than relying on speculation.
Material, treatment and aging limits you should expect
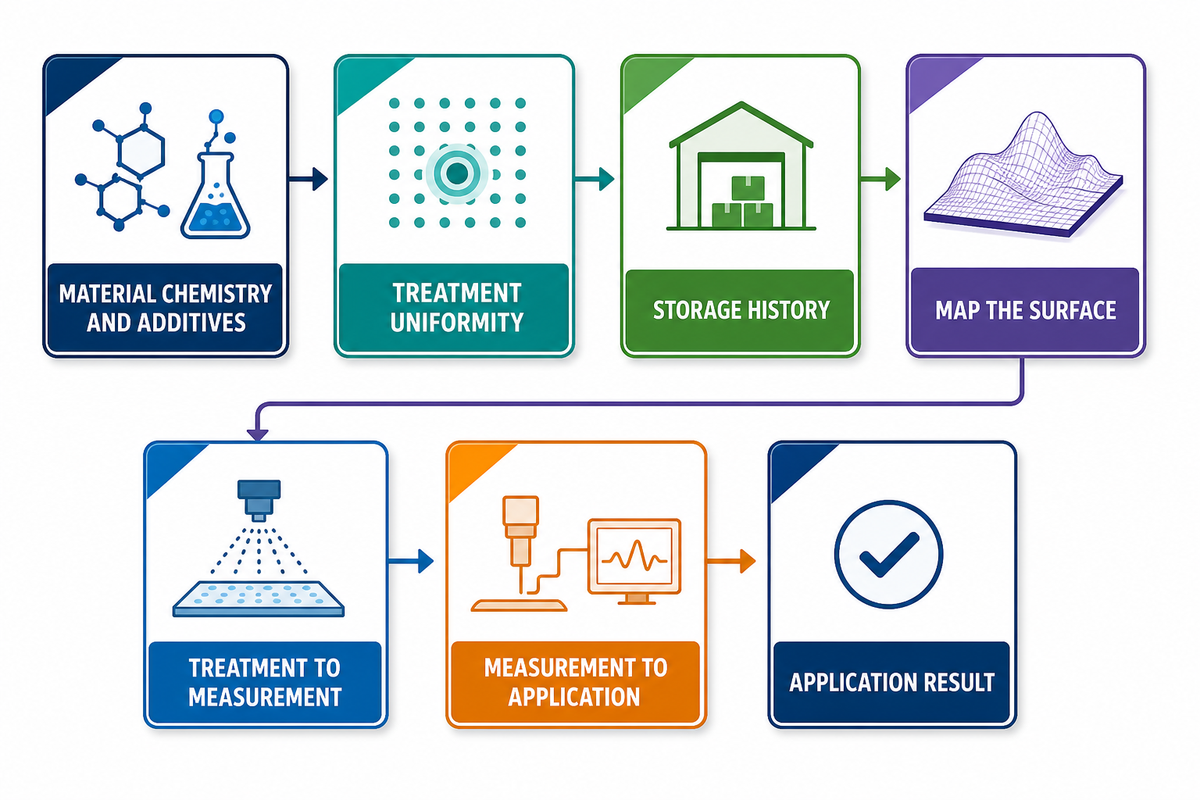
Wetting is a surface condition rather than proof that one surface will bond to another. It depends on material chemistry, additives, fillers, porosity, treatment and surface texture. It can also depend on treatment uniformity and storage history. A treatment gradient is possible on a roll. On a molded part, the gate, weld line and textured face can behave differently. On a coated surface, the coating’s top layer may dominate the reading even when the substrate is unchanged. A marker or pen touches only a small area and cannot guarantee treatment uniformity. Map the surface when uniformity matters, and use an application result for a release decision.
Polyolefin filmUse the ASTM D2578 scope carefully, note the film side and correlate with the actual ink, coating or adhesive.
Porous or textured partsAbsorption and geometry can make a visual continuity rule less reliable; document the method limitation.
Treated surfacesRecord treatment-to-test time. A fresh reading after corona treatment is not automatically the shipped-part reading.
Stored rolls or partsTrack packaging, dust, migration, humidity and handling. “Same resin” does not mean “same surface.”
When a team asks for a “minimum dyne value,” several questions can be used as alternatives. “For what material and side?” “After how much aging?” “For what application result?” Answering these questions provides more information than stating a random number. Moreover, stating a number creates an understood contract between the process and the team members. The contract supports an easy verification of a process when the system changes. Loss of immediate bond isn’t the only outcome associated with a later change in surface wetting. Other factors, such as time, age and environment, may influence a later screen without proving immediate bond loss.
The two clocks on the traveller are treatment-to-measurement and measurement-to-application; together they show when the screen was taken and whether the tested state was still present when bonding or coating began. If the time intervals aren’t documented, the validation should be considered a diagnostic observation rather than a release claim.
A process can define continuity for a stated observation window. Record that window on the traveller. Two-Second Timer Rule: if your procedure uses a two-second observation, print that rule on the traveller and train every operator to use the same timer. If the time window changes, the meaning of the number changes with it.
Dyne Test Screen Escalation Boundary: when to trust the screen and when to escalate
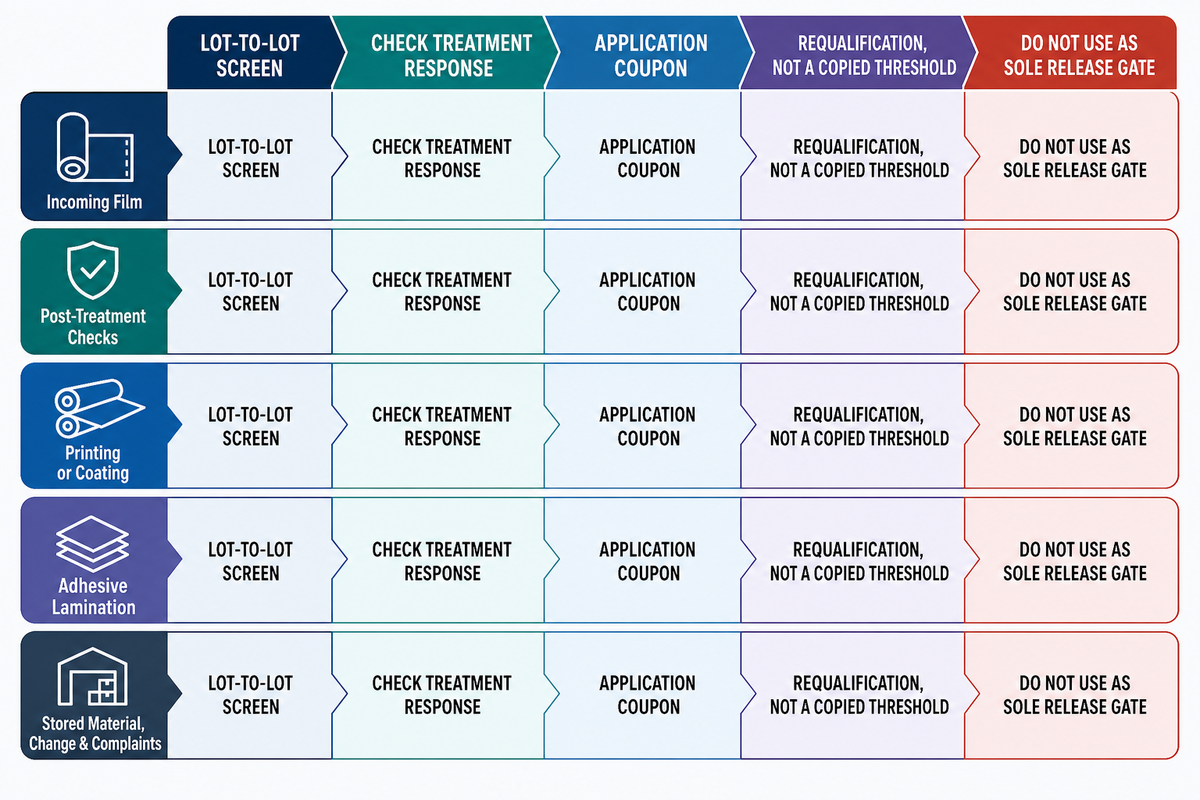
The following list and table outline the distinctions between screening and release decisions. The boundary is conservative: because the dyne test is correlated only to stated materials, method-defined observation windows and process conditions, a factory must escalate a result outside the qualified window to an application test rather than treat it as a release specification.
| Situation | Dyne test role | Escalation trigger | Evidence needed next |
|---|---|---|---|
| Incoming film lot comparison | Fast lot-to-lot screen | Value outside the qualified window | Supplier record, repeat map and application coupon |
| After corona or plasma treatment | Check treatment response | Direction or roll-position variation | Cross-web map and treatment settings |
| Before printing or coating | Check wetting readiness | Ink beads or print adhesion fails | Ink-specific print test and surface cleanliness check |
| Before adhesive lamination | Screen a known surface state | Peel or shear fails despite a pass | Adhesive compatibility, cure and failure-mode review |
| Stored treated material | Trend aging | Value drifts with time or packaging | Time-series samples and storage-condition log |
| New resin, additive or supplier | Detect a surface change | Baseline no longer predicts application | Requalification matrix, not a copied threshold |
| Textured, porous or absorbent surface | Use with method caveat | Visual result is unstable or ambiguous | Contact-angle or application-specific method |
| Customer complaint | One clue among several | Dyne result conflicts with field failure | Retained sample, contamination check and bond failure analysis |
| Release decision with no correlation data | Do not use as sole release gate | Any high-consequence decision | Validated application test and documented acceptance plan |
Common dyne-testing failures and how to troubleshoot them
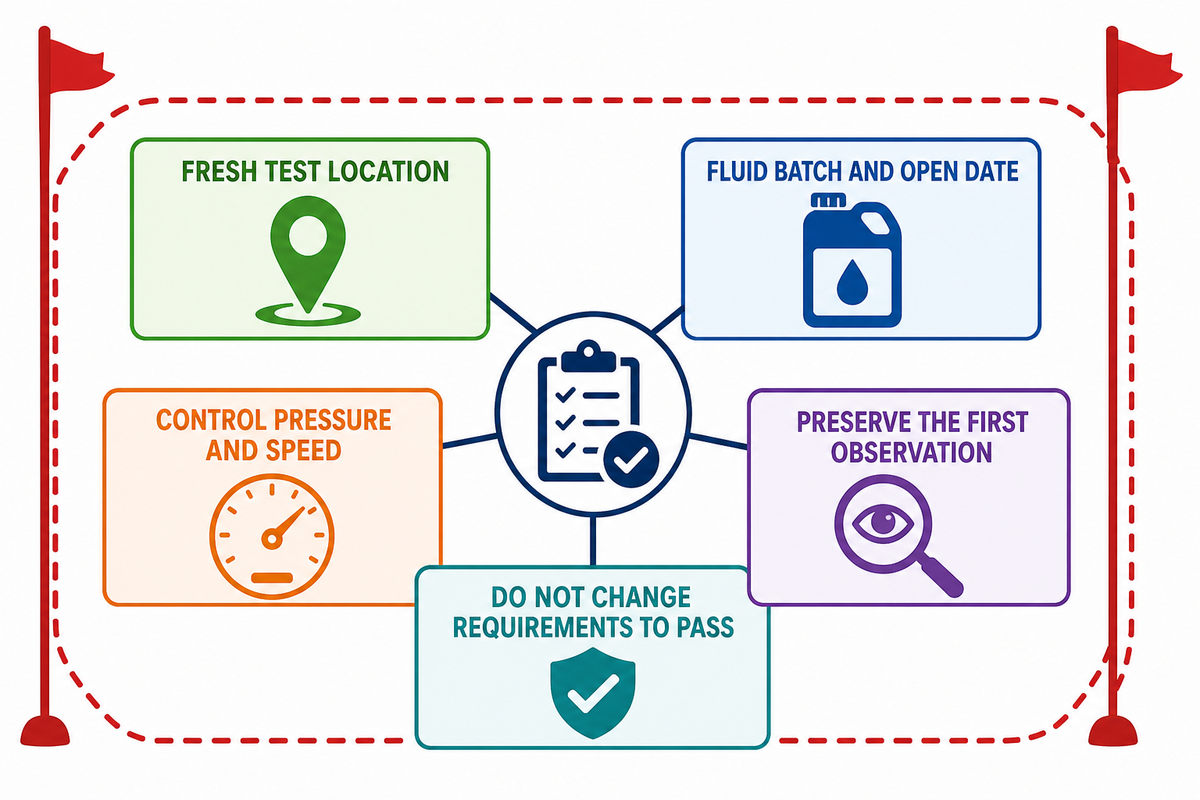
The main reason for bad test results isn’t poor arithmetic; it is uncontrolled method conditions. Results are often interpreted beyond their limitations because a factory team has not controlled the surface, test liquid or operator method, or repeated a failed screen before disposition.
- Dirty test zone: The test zone must be evaluated using a fresh location and a review of glove, wipes and packaging contact. Ink condition is checked separately in the next item. Do not use a more rigorous cleaning agent until the chemistry and reason for use are documented.
- Old or open ink: verify cap closure, batch and open date; a reference surface can expose a fluid that has changed.
- Methods must be carefully controlled, and operators must be trained to understand pressure and speed.
- Wrong side or wrong material: Review the lot and label to make sure the correct side of the material being evaluated has been utilized.
- Over-reading a borderline line: call it borderline, repeat, and preserve the first observation rather than rounding it up to the nearest “pass” level.
- Different methods must not be compared as if they were the same.
- Ignoring elapsed time: add a treatment-age field to the record. “Tested today” is not enough for a stored roll.
- Just because a market demand exists, it doesn’t mean that your materials are properly specified.
Common mistake: Reviewing the qualified method and application requirements should identify issues; changing the test liquid until the surface passes instead moves the goalpost. Do not change the requirements simply to attain a pass.
What to record so the result can be repeated
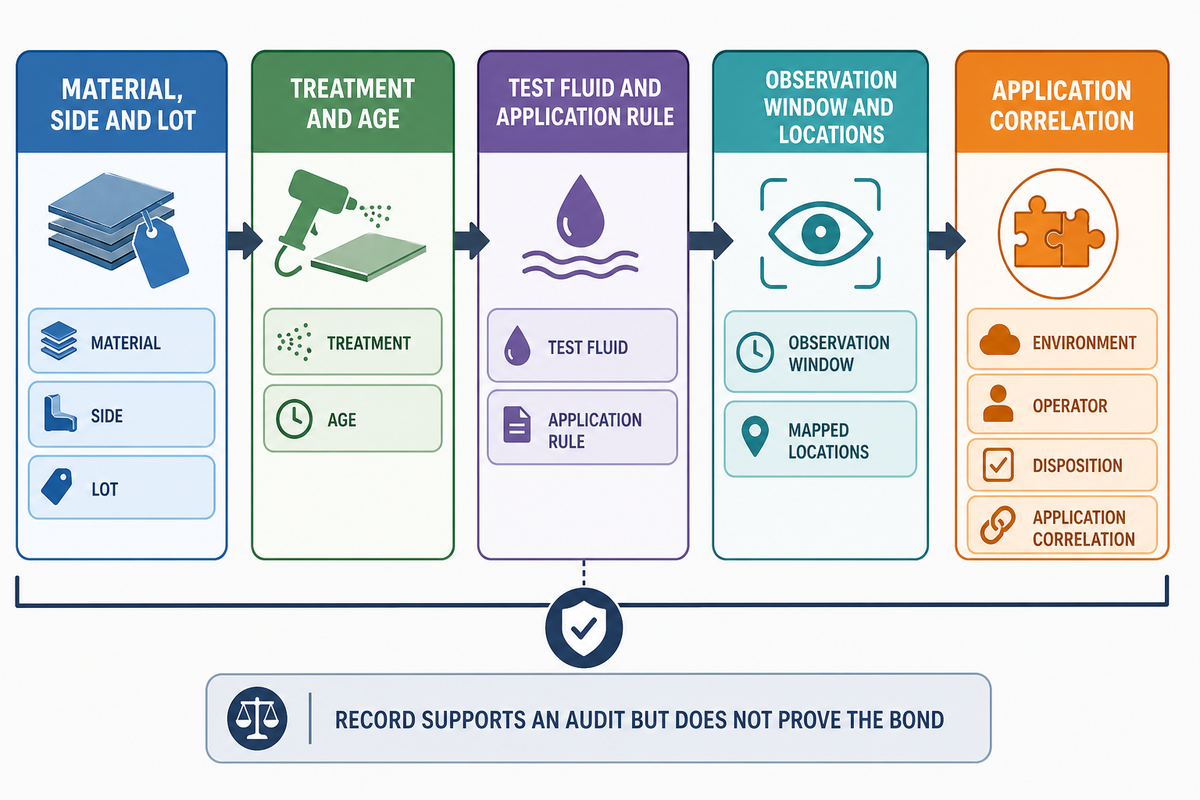
Results of tests performed outside prescribed conditions have little evidentiary value; because a factory quality team needs an auditable record, document the test liquid, material, procedure-defined observation window, treatment age and production lot before release. The following fields let production and quality-control teams audit the data without treating the screen as bond proof.
| Record field | Example format | Why it matters |
|---|---|---|
| Material and side | PP film, treated side, lot 24A | Different sides and lots can wet differently. |
| Treatment and age | Corona, 6 h after treatment | Surface state can change with time. |
| Test fluid | Pen or ink grade, batch, open date | Fluid condition is part of the measurement. |
| Application rule | Stroke length, volume, direction | Operator technique affects the visual result. |
| Observation window | Continuous for 2 s; breakup at 4 s | Timing prevents vague pass language. |
| Locations | Machine direction, cross direction, 3 points | Maps non-uniform treatment or contamination. |
| Environment | Temperature, humidity if controlled | Explains variation when the process is sensitive. |
| Operator | Initials and training revision | Supports repeatability and coaching. |
| Disposition | Release, hold, repeat, application test | Connects the screen to a controlled action. |
| Application correlation | Peel, print or coating result ID | Shows whether the screen predicts what matters. |
In the absence of the application result, a wetting screen would not constitute proof of adherence to the requirements. For quality assurance, the substrate (i.e., the materials) should be named, the ASTM method should be cited, and the time of the test with respect to surface treatment should be stated.
From reading to bonding evidence: a practical decision framework
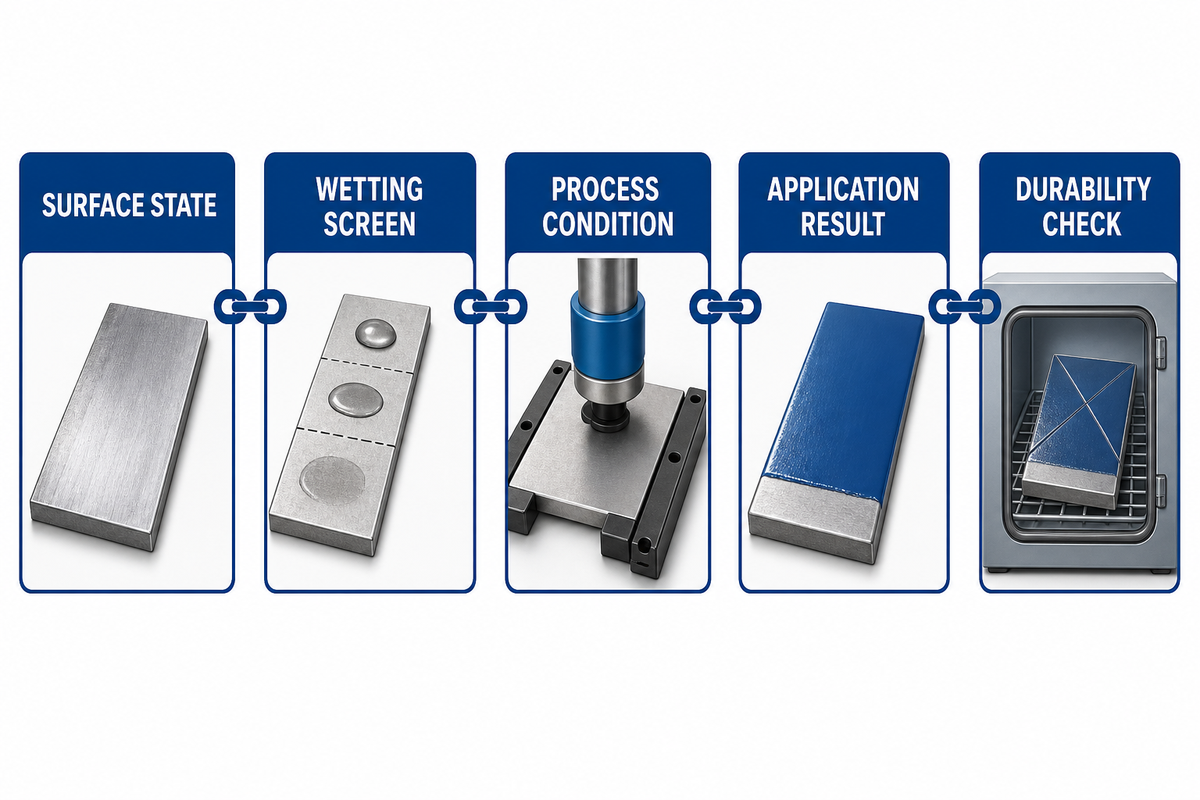
The Reading-to-Bond Evidence Chain should be applied to keep decisions proportionate; each link answers a different question, and no inference should exceed the evidence at that link.
- Surface state: What surface conditions and age were tested?
- Wetting screen: Was the wetting screen used according to instructions?
- Process condition: Were the factory process conditions, cleaning, pressure, temperature and speed controlled under the written method so that the procedure-defined observation point is reproducible? Was the cure complete?
- Application result: Did the actual ink, coating or adhesive meet its performance test?
- Durability check: Would the item being tested meet the required standard after normal use or storage?
Link 2 of the chain represents the wetting-screen result for the material, not a direct measure of surface energy. If this fails, the surface or method should be reviewed before the process moves to link 3. If link 3 fails, the process and chemistry of the material should be reviewed. Link 4 of the chain is the application result; it does not represent maximum and minimum allowable dyne levels. If link 4 fails, the application test should be reviewed with the material chemistry, cure, contamination, pressure and actual failure mode.
This framework does not require a converter or printer to disclose trade secrets. A supplier can report a measured dyne range without claiming that the range guarantees the customer’s bond, while the converter still requires a print, coat or laminate trial.
FAQ: dyne test questions from production and quality teams
Is a higher dyne test result always better?
No. A higher result can indicate easier spreading of the chosen test liquid, but the useful question is whether the value predicts the actual ink, coating or adhesive process. Material chemistry, treatment age, contamination, cure and service exposure can control the final result. Build the acceptance window from correlated samples and state the method, liquid, observation time and material. Treat a generic “higher is better” chart as a starting hypothesis, not a release specification.
What does 38 dynes/cm mean in a dyne test?
At 38 dynes/cm, the result means the surface accepted the labelled test liquid under the stated procedure and observation window. It doesn’t mean every adhesive will bond, and it doesn’t prove compliance for every material. The often-quoted 38 dynes/cm value isn’t a universal pass line. Confirm the substrate, the test-fluid family, the edition and scope of the method, then verify the result with the application test that measures your real risk.
How long does a dyne pen result remain valid?
The result is valid for the sample state and method conditions you recorded, not for an unlimited calendar period. Treated polymer surfaces can change with storage, handling, migration, humidity and elapsed time. A pen or ink can also change with age, contamination or poor closure. Record treatment-to-test time and fluid batch, then establish your own recheck interval by comparing fresh and stored samples against the application result. Don’t promise a shelf life from the dyne number alone.
In a controlled study, retain a reference strip and repeat the screen at the planned storage checkpoints; that creates evidence for your own packaging and treatment window rather than borrowing a number from a catalogue. Include the same application coupon at each checkpoint, keep the operator instruction unchanged, and document any cleaning or conditioning step. This turns “valid for 30 days” from an assumption into a result that another team can reproduce and challenge.
Can I use a dyne test on every plastic?
You can often use a wetting screen as a diagnostic, but the method and interpretation depend on the plastic, surface texture, additives and whether the surface is porous or coated. ASTM D2578 is specifically associated with wetting tension of polyethylene and polypropylene films.
Other substrates may need a different liquid system, contact-angle method or application-specific test. If the line is unstable, verify material identity and method scope before changing the process target.
Why did the dyne test pass while the adhesive bond failed?
The screen answered a wetting question, while the bond failure may have come from adhesive compatibility, cure, pressure, contamination, cohesive weakness, thickness, temperature or aging. Review the failure surface and compare the dyne record with the adhesive lot and process settings.
Run a controlled application coupon and retain the sample. The right conclusion is often “wetting was adequate; another variable controls the bond,” not “increase the dyne target until the failure disappears.”
Need a film and bonding decision that supports production review?
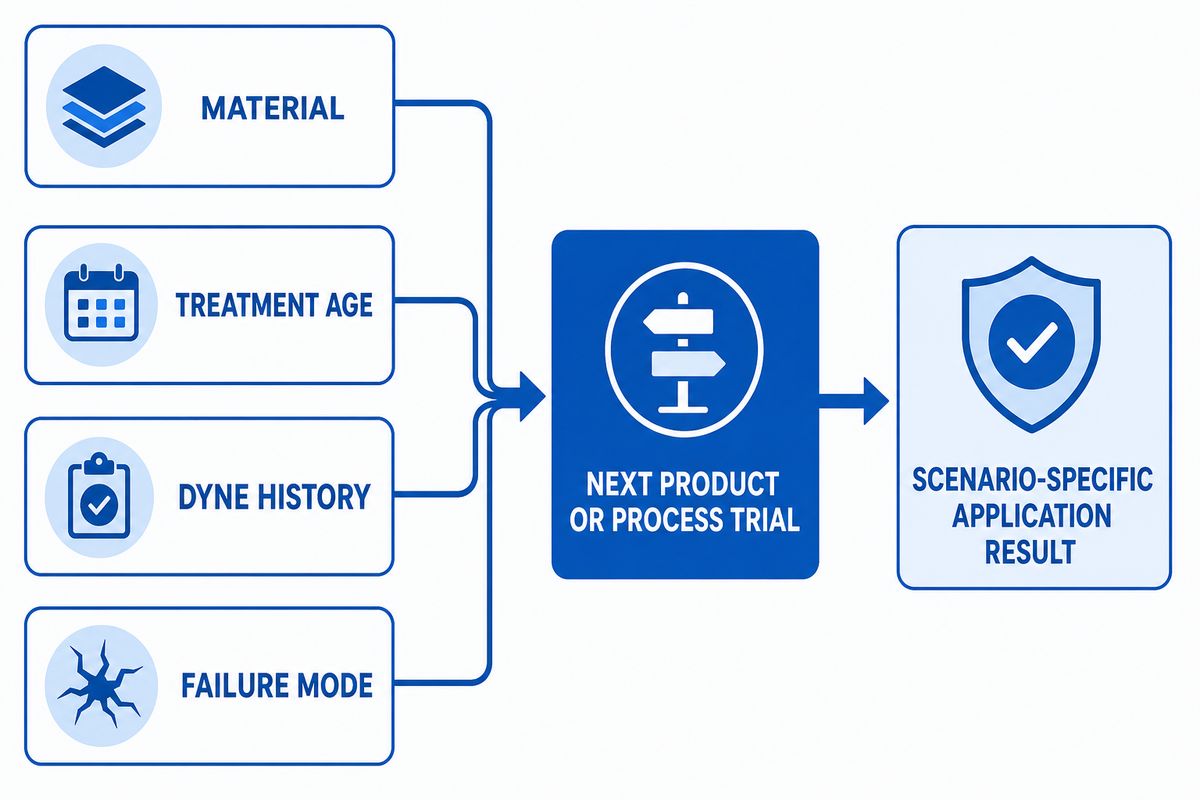
Consider all the evidence including material, treatment age, dyne history, and failure mode before setting a threshold; because a factory review needs a scenario-specific application result, use the screen to select the next product or process trial rather than relying on it alone. In the absence of evidence, a screen captures very little.
References & Sources
The following references provide standards scope or applied measurement context. Brighton Science, Tantec and Enercon are commercial vendor technical guidance; third-party material does not establish Tengyang ownership, certification or grade performance.
- ASTM D2578 method record wetting-tension scope for polyethylene and polypropylene films. For edition tracking, see the ASTM D2578-23 catalogue record.
- ASTM public D2578 page standard record and scope context.
- Brighton Science: What Is Dyne Testing? Procedure and practical limitations.
- Tantec UK: How to Use Dyne Pens and Test Inks applied handling context.
- Enercon: Using Dyne Solutions and Dyne Pens non-porous substrate context.
- Brighton Science: Demystifying Dyne Levels contamination and interpretation limits.
- Enercon corona treating overview: mention about directional treatment and end-product caveat.