Get in touch with Tengyang Company

Technical Surface Specification
Corona Treatment: Surface Activation and Aging
Match corona treatment with the adhesive and bonding process your film will actually use. Shanghai Tengyang supplies hot melt adhesive films, webs, powders and granules, with material selection and application support for industrial lamination.
A usable surface reading needs a bonding result
Corona treatment can improve polymer wettability, but a low contact angle does not establish a durable bond. Check the treated side, elapsed storage time and laminate performance together before changing your material specification.
SPEC-01
Adhesive forms
Films, webs, powders and granules
SPEC-02
Film material families
TPU, EVA, PA, PES and PO
SPEC-03
Customization support
Thickness, width, melting point, color and application-specific formulations
×
![Full Screen View]()
Surface Activation for Hot Melt Adhesive Bonding
A film that an adhesive does not wet out is difficult for that adhesive to contact consistently. Corona surface activation alters the outer polymer surface; the adhesive must still be compatible with the film chemistry, service conditions and available heat and pressure.
Corona treatment process variables
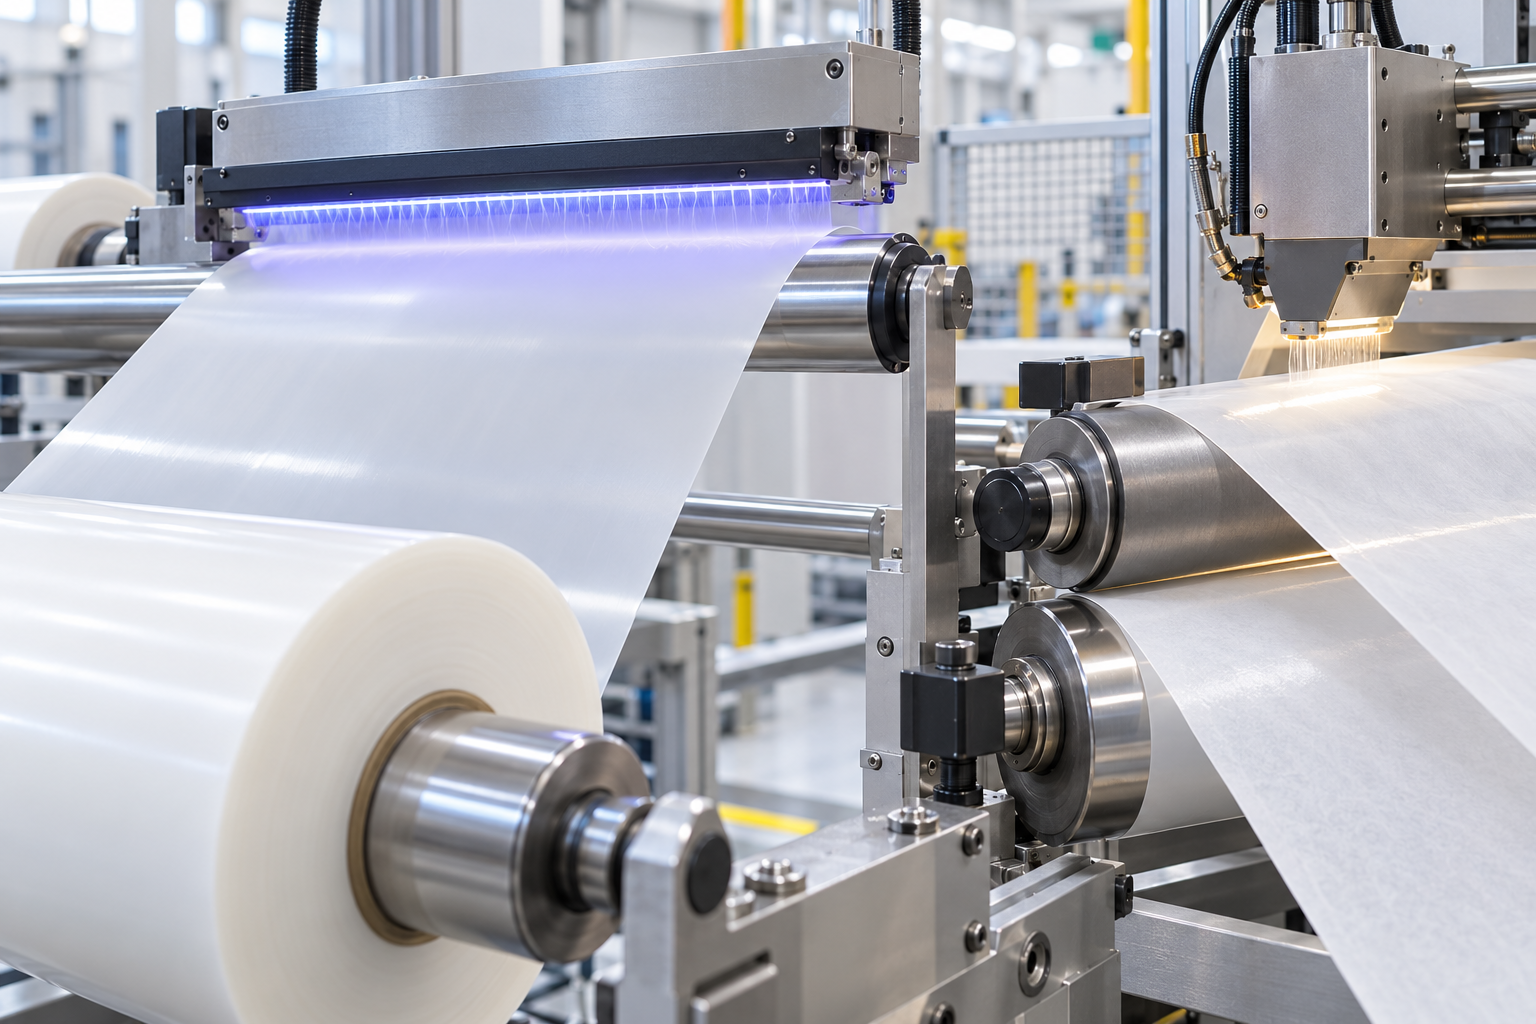
A corona treatment system uses a generator and high-voltage electrode configuration to ionize a gas near the moving web. The corona discharge generates a reactive plasma, while the dielectric barrier helps control the discharge; line speed, treated width and delivered power affect exposure.
Surface chemistry
Oxidation can increase the surface energy and alter how a liquid spreads.
Web conditions
Wrinkles, electrode spacing and contact with the support roll influence treatment uniformity.
Bonding conditions
Hot melt temperature, dwell time, pressure and cooling determine adhesive contact and retention of surfaces.
Adhesive selection starts with your process
We support hot melt material selection for garments, footwear, leather lamination, automotive interiors, packaging and other industrial bonding applications. Send the substrate construction and processing limits so we can recommend a suitable adhesive material for your production. Corona treatment is not a substitute for selecting an adhesive that can bond within those processing limits.
Polymer Films and Hot Melt Adhesive Selection
Identify the exposed bonding surface, including any coating, printing ink or release layer. For a converter combining extrusion, printing and lamination, the outside face at each operation counts: a polyethylene core does not make the outside of a multilayer film polyethylene. Different treatment responses for PE, PP and PET were observed in a polymer-film study; compare the actual grade under matched conditions.
Substrate details for material selection
Polyethylene film
Specify: Grade, additives, blown/cast construction, treated side.
Compare: Wetting and bond results on actual grade.
Polypropylene / BOPP film
Specify: Orientation, slip additives, print/bond face.
Compare: Treatment response and laminate failure.
PET or coated film
Specify: Exposed polymer/coating, surface history.
Compare: Method suitability & adhesive compatibility.
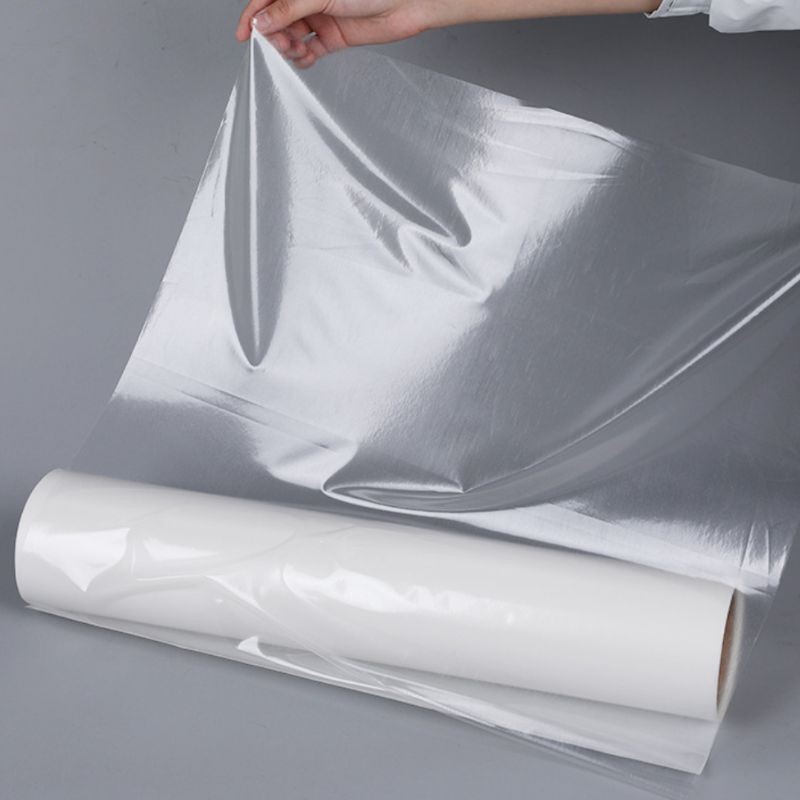
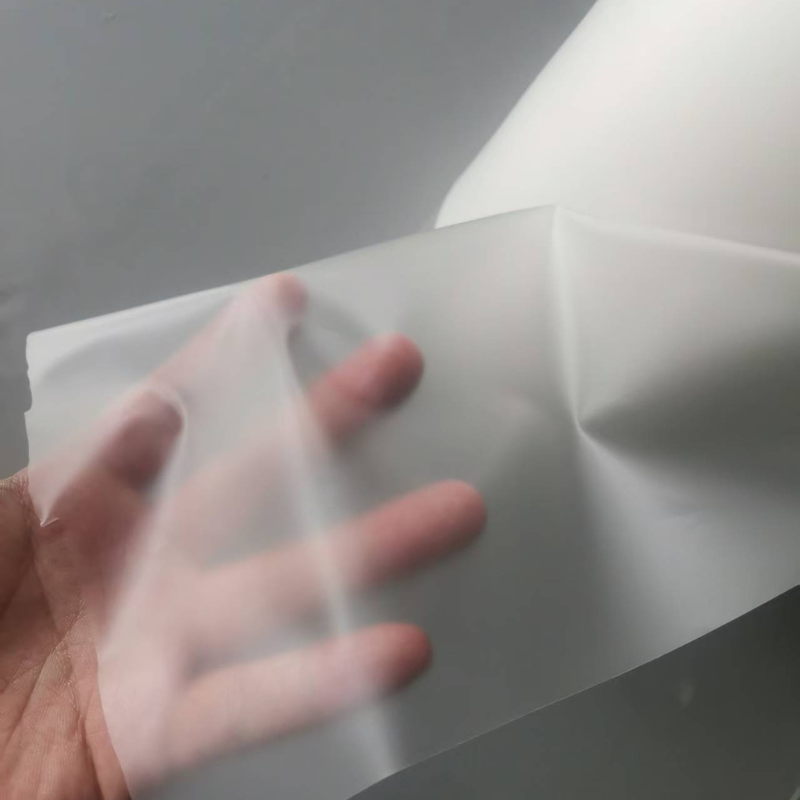
Transparent adhesive film unrolled from a client-supplied sample roll. Adhesive film sample from the Tengyang product image library.
Our hot melt adhesive film range
We supply TPU, EVA, PA, PES and PO hot melt adhesive films. Select a grade against the complete material stack and service requirements; the polymer family name alone does not specify bonding temperature, wash resistance or peel strength.
TPU
Flexibility, stretch, hand feel and compatibility.
EVA
Available process temp, flexibility and end use.
PA
Bond performance, service exposure, process window.
PES
Substrate pairing, dimensional requirements, service.
PO
Polyolefin surface compatibility and complete process.
Film options for the bonding trial
Our polyester TPU and EVA film options provide dimensional and activation ranges. [ DATAPAD 1 / 3 ]
Surface Treatment Aging Before Lamination
A corona treated roll can change between treatment and use. Surface treatment aging can involve polymer segment reorientation, additive migration and contamination, so the original treatment level needs a date and a storage history.
Polymer response
PE, PP and PET do not share a single decay curve. Film grade and processing history belong in any comparison of surface energies.
Storage conditions
Record temperature, humidity, packaging and exposure to handling or dust. Additives can migrate toward the surface, changing the interface that will meet the adhesive.
Time before bonding
Record when the film was treated, measured and laminated. Use matched samples and the same measurement procedure to separate elapsed time from test variation.
Recheck stored film at the point of use
Match a retained reference with the film entering production, then produce the intended laminate at recorded conditions. Decide whether to use, modify or retreat the material from those data; a roll label alone cannot determine its current bonding performance.
- Keep the treated side and sampling locations consistent.
- Record each individual reading and the mean and spread.
- Test a proposed in-line refresh setting before applying it to a production roll.
QC VALIDATION // PASSED
More treatment can be the wrong correction
Higher dose does not guarantee higher bond strength: a film-lamination study using polyurethane adhesive found a loss of strength after overtreatment in its BOPP samples. Investigate a weak surface layer or adhesive mismatch when wetting improves but adhesion does not.
OVER-DOSE ALERT // SYSTEM CHECK
Contact Angle, Wetting Tension
and Bond Tests
A wetting-tension result is not a substitute for a bond test. Unlike a surface reading, the laminate test assesses the selected adhesive and assembled structure; record both results against the same material history.
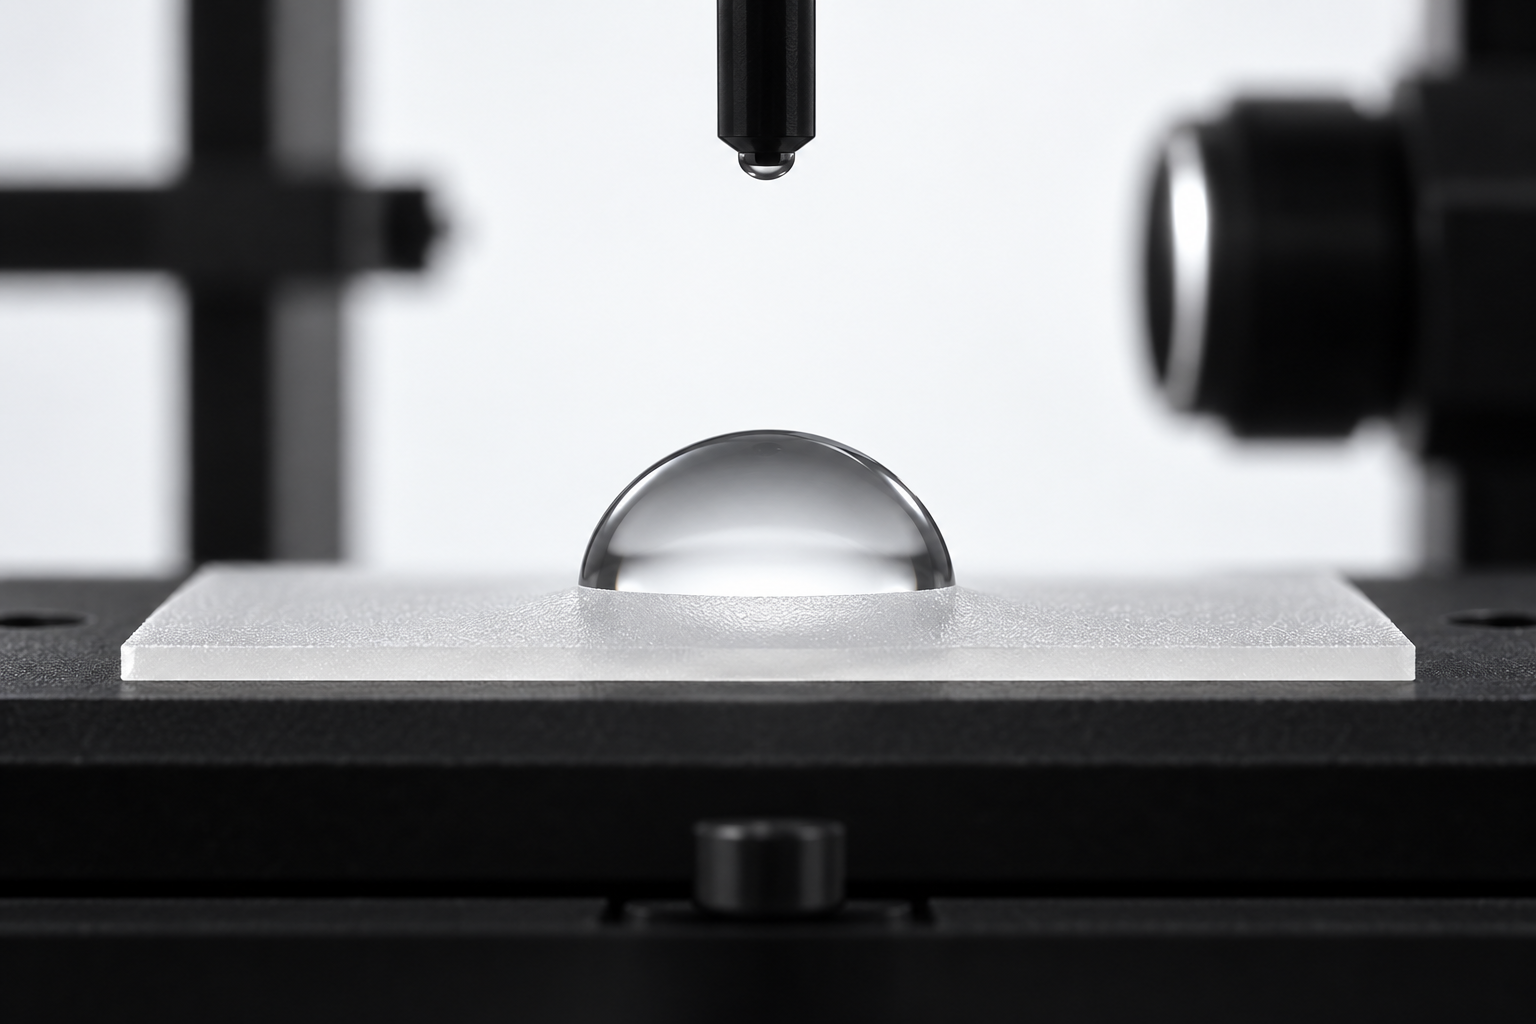
Use each test for the question it answers. Water contact angle, dyne testing and mechanical bond testing describe different parts of the interface, and cannot replace each other.
Measurement choice and interpretation
Water contact angle
Drop angle on a defined surface at a stated reading time.
ASTM D5946-24 addresses corona-treated polymer films; method and spatial variation matter.
ASTM D5946-24 addresses corona-treated polymer films; method and spatial variation matter.
Wetting tension / dyne level
Wetting behavior with specified test liquids.
ASTM D2578-23 covers PE and PP film; establish applicability before using it on other polymers.
ASTM D2578-23 covers PE and PP film; establish applicability before using it on other polymers.
Calculated surface energies
Model-based estimates using defined probe liquids and assumptions.
Compare surface energies only with the model and liquids recorded; a single water angle does not uniquely determine polar and dispersive components.
Compare surface energies only with the model and liquids recorded; a single water angle does not uniquely determine polar and dispersive components.
Peel or other bond test
Mechanical response of the actual adhesive/substrate construction.
Keep specimen preparation, geometry, speed, conditioning and failure-mode classification consistent.
Keep specimen preparation, geometry, speed, conditioning and failure-mode classification consistent.
Keep the two acceptance decisions separate
A high surface energy reading is only part of the check.
ASTM D5946-24 and ASTM D2578-23 both caution against using their surface measurements alone to establish acceptable adhesion. Compare the resulting laminate against the bond and service requirements agreed for your application.
The Side–Time–Bond Check
Use this record to correlate a surface measurement with the material and bonding trial it reflects. Sample across the width and along the machine direction as per your agreed plan, retaining repeat readings rather than reporting only the best point.
Information to record before comparing samples
Material identity
Supplier, polymer grade, lot, roll and exposed surface
Surface history
Treated side, treatment date/time, prior cleaning or coating
Treatment settings
Equipment, delivered power, width, speed, electrode gap and number of treated sides
Storage
Elapsed time, temperature, humidity, packaging and handling
Sampling
Width position, machine-direction position and repeat count
Contact-angle method
Liquid, drop volume, reading delay, instrument settings and individual angles
Wetting-tension method
Liquid identity, condition, application method and observation time
Bonding trial
Adhesive grade/form, coat amount or thickness, heat, pressure, dwell and cooling
Bond result
Specimen width, test geometry and speed, conditioning, strength and failure mode
Hot Melt Adhesive Selection and Project Quotations
We support OEM requirements and customized thickness, width, melting point, color and application-specific formulations. For a useful quotation, send the material construction, adhesive form, quantity and delivery requirement together. Include the intended bond test: ASTM D5946-24 does not establish adhesive retention from a contact angle alone.
Compare the complete bonding requirement
| Quotation input | Why it matters | What to send |
|---|---|---|
| Material and form | Film, web, powder and granules have different application requirements | Current adhesive and application equipment |
| Thickness or coating amount | Adhesive usage affects material cost and the finished laminate | Target thickness or mass per area, plus allowable variation |
| Width and quantity | Roll layout, conversion and order scale affect the supply requirement | Usable width, trial quantity and expected repeat demand |
| Performance and schedule | Material selection and trial needs must fit the intended application | Bond criteria, service conditions and required delivery date |
ASTM D5946-24 PROTOCOL VERIFIED
Trial material before a larger order
Include your trial roll or sample requirement in the enquiry. Agree the selected grade, specification, order quantity and delivery schedule before placing the production order.
- Compare material consumption per usable bonded area.
- Track rejected laminate and rework alongside adhesive purchase cost.
- Keep experimental treatment changes separate from confirmed production settings.
Corona vs Plasma Treatment and Other Preparation Routes
Choose the next trial from the failure mode
Corona and a primer are not interchangeable process steps: one modifies the exposed surface, whereas the other introduces an additional material whose compatibility must be tested. The trade-off with a primer is the extra application and activation step; evaluate whether the resulting bond improvement justifies it for the laminate.
Select the preparation route for the actual substrate, adhesive and production geometry. Plasma treatment results can be adhesive-selective even within a controlled polymer comparison, so a technology name is not a bond specification.
What to evaluate
Web handling, one- or two-side exposure, dosage and elapsed time
Trial question
Does the intended plastic film laminate meet its bond criteria across the sampled roll?
What to evaluate
Source design, gas, exposure pattern and surface chemistry
Trial question
Does the tested process suit this adhesive and substrate combination?
What to evaluate
Compatibility, application amount, activation or drying needs
Trial question
Does adding the primer improve the required bond without unacceptable process changes?
What to evaluate
Contaminant identity, surface sensitivity and resulting cleanliness
Trial question
Has the cause of poor bonding been removed, or has only the reading changed?
From Material Details to a Bonding Trial
Tengyang film production and material support
Our polyester TPU film is manufactured on an in-house casting and slitting line. Our EVA film production includes in-house material testing, compounding, cast and blown film extrusion, coating, slitting and rewinding. Bring your trial results into the material discussion so the adhesive recommendation addresses the failure observed on your line.
PHASE 01
Describe the layers
Send the substrate names, exposed surfaces, thicknesses and end-use.
PHASE 02
Record your process
Include treatment history, available bonding temperature, line speed, dwell time and pressure.
PHASE 03
Discuss adhesive selection
We provide material selection and application support for the required bonding task.
PHASE 04
Specify the trial
Confirm the sample requirement and test the selected material under your planned production conditions.
PHASE 05
Compare the trial outcomes
Retain surface readings, laminate results and service condition checks together when reporting the trial. ASTM D2578-23 treats wetting tension as an incomplete measure of adhesive adhesion.
PHASE 06
Order confirmation
Establish the grade, dimensions, quantity and delivery plan for the approved structure.
"Tell us your material, bonding process, temperature, width, thickness, and application requirements."
Shanghai Tengyang New Materials Technology Co., Ltd.
When Surface Activation Alone Is Not Enough
To accelerate troubleshooting, assess where the bond failed before escalating treatment levels. A low surface energy substrate can be one of many problems; weak coatings, mobile additives, inadequate adhesive flow and incompatible materials all require their own evaluation. A polyurethane-laminated film study found reduced bond strength after overtreatment of its BOPP samples, supporting a trial before increasing exposure.
01
Good wetting, weak bonding
Consider adhesive selection, processing conditions and whether failure occurs in the surface layer or the adhesive.
02
Different results across the roll
Check for contamination, treatment uniformity and sample positions.
03
Bond loss after conditioning
Analyze the entire structure against its heat, moisture or other field exposure.
04
Unstable results after storage
Compare retained and at-use samples before choosing a refresh treatment.
Surface Science & Measurement Tools
Contact Angle Summary
Comprehensive overview and evaluation metrics for surface energy and contact angle measurement in industrial adhesive applications.
Film Usage & Preparation
Guidelines and tracking matrices for treating, storing, and preparing plastic films before hot melt lamination processes.
Treatment Dose Calculator
Calculate and optimize the required corona treatment dose parameters for various polymer substrate materials.
Corona Treatment Questions for Film Bonding
There is no single storage interval that guarantees bonding performance for every treated film. Polymer grade, additives, treatment conditions and storage history affect decay; remeasure at use and confirm the laminate under the intended process.
Set acceptance criteria for the actual adhesive, substrate and test method. A lower water angle indicates different wetting under the same test conditions, but ASTM D5946-24 does not make that reading a complete adhesion test.[3] When your report includes calculated surface energies, retain the probe liquids and calculation model.
Agree a material- and process-specific wetting requirement alongside the bond test. A target used for printing inks or an ink coating should not automatically become the acceptance limit for a hot melt laminate.
Specify each face by its next operation: printing, coating or adhesive bonding. Confirm the treated side with the film supplier, and check the relevant face during your trial; both-side treatment is not a universal requirement.
Check the adhesive-facing surface and test the actual laminate. Corona treatment for printing addresses an ink application; your hot melt process still needs its own material and bond acceptance criteria.
Evaluate a proposed refresh process on the actual material before using it for production. Record the earlier treatment and storage history, then compare wetting and bond performance because additional exposure can change the surface in unwanted ways.
Yes. A treated-film label does not guarantee compatibility with your ink or adhesive.
Changing speed changes exposure when delivered power and treated width stay fixed. Record all three variables and the equipment configuration; corona treaters should be compared using their actual treatment conditions, not voltage alone.
Send your substrate construction, application, adhesive form, temperature, width and thickness requirements. Add treatment history, existing trial results, expected quantity and delivery needs so we can discuss a suitable hot melt material. When a previous laminate failed, include the separation location and the conditions before failure, such as storage or washing, to help focus the material discussion.



